A molded elastomer changes shape as compound flows, the mold closes, rubber cures, and the part cools. Flash removal and measurement force add further variation. Applying machined-metal limits to that process produces expensive disputes without necessarily improving fit. Useful rubber tolerances protect sealing, location, and assembly while acknowledging how the feature is created.
This drawing guide is for engineers and buyers specifying molded seals, boots, bumpers, diaphragms, and insert-bonded components. It explains how to classify dimensions, place datums and parting lines, define measurement methods, and review rubber tolerances before tooling.
Table of Contents
Classify Rubber Tolerances by Mold Control
A dimension formed within one mold plate is controlled differently from a thickness spanning the mold closure. Insert location, trimming, and post-cure can introduce other variation. Mark each critical feature as fixed-mold, closure-dependent, insert-controlled, or trimmed. This lets the manufacturer explain realistic rubber tolerances using the intended tool construction.
Then rank dimensions by function. Sealing bead height, insert position, and mounting-hole relationship may be critical; a noncontact outside edge may not be. Use general limits for noncritical geometry and explicit controls only where deviation changes assembly or performance.
Put the Parting Line Where Variation Is Acceptable
The mold must separate, and compound can create a thin fin where sections meet. Route that boundary away from sealing lips, sliding surfaces, optical areas, and high-strain flexures when geometry permits. The parting line also influences draft and tool access. Rubber tolerances near that boundary should include an agreed flash and mismatch definition.
Do not specify “no flash.” State maximum extension, thickness, or functional effect and identify the measurement region. The rubber molding process guide discusses parting-line and trimming choices in greater detail.
| Feature type | Primary source of variation | Drawing response |
|---|---|---|
| Cavity length or width | Mold size and compound shrinkage | Dimension from stable molded datums |
| Closure thickness | Mold closure and compound volume | Allow process-appropriate thickness range |
| Insert location | Fixture and insert movement | Datum to functional insert surfaces |
| Trimmed edge | Flash-removal method | Define edge condition and trim limit |
Select Datums That Can Be Reproduced
A soft free-form surface may not sit the same way twice. Choose molded pads, insert faces, locating bosses, or a defined restrained condition that reflects installation. If the part is measured on a fixture, show support points and clamping force. Otherwise, apparent failures in rubber tolerances may be caused by different setup rather than different parts.
For endless profiles or large flexible components, distinguish free-state dimensions from installed dimensions. Specify permitted stretch and the method used to establish perimeter, rather than forcing a limp part flat against an undefined table.
Account for Compound Shrinkage Before Tool Release
Shrinkage depends on polymer, formulation, cure, part geometry, flow, and tool temperature. It is not a universal percentage for “rubber.” The manufacturer applies an expected allowance to the tool and may adjust after initial samples. Tight rubber tolerances across large dimensions can require trial correction and should be justified by function.
Changing compound after tooling can change shrinkage and fit. If several materials are being evaluated, identify which geometry risks can be tested in a prototype and which require production-intent tooling. Record any tool correction and associated drawing revision.
- Identify the exact compound or performance family.
- Flag closure dimensions and insert-controlled features.
- Define free-state or restrained inspection.
- Locate flash and mismatch limits on the drawing.
- Link tight rubber tolerances to a stated assembly function.
Dimension Holes, Lips, and Undercuts by Process
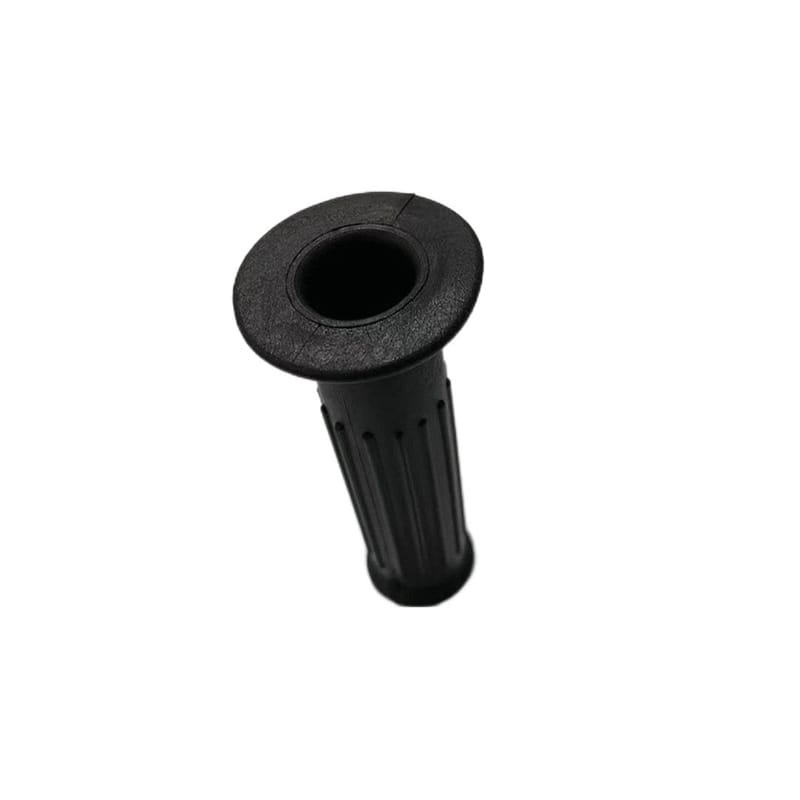
A molded hole may require a core pin and can show flash or deformation at its opening. A punched hole has a different edge. Thin lips need tool support and may be affected by tear trim. Undercuts can demand a flexible demold path or split tooling. Review how each feature will be formed before assigning rubber tolerances.
Where a hole only clears a fastener, avoid locating it more tightly than the assembly requires. Where it positions an insert or controls fluid flow, define the datum relationship and inspection method. The custom molded rubber parts page shows custom molded geometries that benefit from early tooling review.
Control Measurement Force and Conditioning
Calipers can compress a soft wall, while a profile projector or gauge may provide a more repeatable result. State the instrument, contact force, fixture, temperature, and time after molding for critical measurements. Hardness and post-cure influence how the part responds. Repeatable rubber tolerances depend on repeatable measurement.
ASTM D2240 covers durometer hardness, while ASTM D3767 addresses dimensions of rubber products. Select the methods relevant to the component and agree how curved or flexible areas will be supported.
Use Appearance Limits That Describe Function
Flow lines, knit areas, small surface marks, and color variation may be cosmetic or may indicate a risk at a sealing or flexing feature. Define zones and defect types rather than using “workmanship acceptable” as the only instruction. A visual standard with approved examples can complement numerical rubber tolerances.
For bonded inserts, inspect exposed metal, rubber coverage, bond-edge condition, and insert movement separately. ASTM D429 may inform adhesion evidence, but the finished component and load direction still need review.
Approve First Articles Against Assembly Risk
First-article inspection should confirm critical dimensions, material identification, hardness, insert location, flash, and visual zones. Then assemble production-intent samples and test sealing, retention, movement, or impact. A perfect report of rubber tolerances does not prove that the part works if the drawing omitted the real interface.
Use ASTM D2000 where rubber classification is appropriate, and keep drawing revision, tool correction, and sample traceability aligned. The rubber gasket design guide helps connect material behavior with tolerance decisions.
When quotations differ, ask each supplier to identify which dimensions drive special tooling, secondary trimming, dedicated gauges, or extended conditioning. This makes the cost of a limit visible without disclosing price in the technical article. An OEM can then decide whether the requirement protects an interface or simply originated from a legacy title block. Keeping a short tolerance rationale beside the design record also helps future revisions avoid tightening a feature that was intentionally left practical.
For families of similar parts, do not assume one tolerance table covers every size and hardness. A small firm component, a large soft boot, and an insert-bonded mount have different handling and measurement behavior. Grouping features by molding control and function creates a reusable drawing strategy while preserving part-specific decisions.
The inspection plan should explicitly connect critical rubber tolerances with the mating assembly and acceptance test. When that relationship is documented, a supplier can propose a gauge or restrained fixture that reproduces use instead of forcing a soft free-state feature into an unsuitable metal-part measurement convention.
Frequently Asked Questions
Why are rubber tolerances wider than metal tolerances?
Molding includes compound flow, cure, shrinkage, mold closure, demolding, trimming, conditioning, and elastic measurement effects. Limits should reflect process and function.
Can rubber tolerances be tightened?
Sometimes, especially on stable fixed-mold features, but tooling, process, inspection, and cost consequences should be reviewed. Tighten only dimensions that protect function.
How are rubber tolerances measured on soft parts?
Define support, restraint, instrument, contact force, temperature, and conditioning. Non-contact measurement or dedicated gauges may be more repeatable than calipers.
Should flash be included in rubber tolerances?
Flash and mismatch should have separate, measurable limits and locations. Avoid an undefined zero-flash requirement.
What drawing information helps quote rubber tolerances?
Provide 2D and 3D files, compound, hardness, critical features, datums, parting-line restrictions, flash limits, inspection state, mating parts, quantities, and functional tests.
Request a Molded Rubber Tolerance Review
Huadao can review custom molded rubber parts for tool split, closure dimensions, inserts, trim access, inspection support, and functional limits.
Send the drawing and mating assembly through the contact page to establish rubber tolerances before tooling assumptions become expensive changes.